Selecting the right valve is one of the most important decisions when designing or maintaining an industrial piping system. If you are wondering how to choose a ball valve, the answer depends on several technical and operational factors including pressure, temperature, media compatibility, installation environment, and maintenance expectations. Choosing the correct valve helps improve operational efficiency, reduce downtime, and extend equipment life.
At Flowlink Valves & Controls, we supply high-quality valve solutions for a wide range of Australian industries. Our extensive product range is designed to meet demanding industrial requirements while delivering dependable performance in critical applications. Whether you require an industrial ball valve for water treatment, mining, manufacturing, oil and gas, chemical processing, or other industrial sectors, selecting the right valve begins with understanding your operating conditions.
This guide explains the key considerations involved in selecting the right ball valve while helping you make an informed investment for long-term reliability.
Understanding the Purpose of a Ball Valve
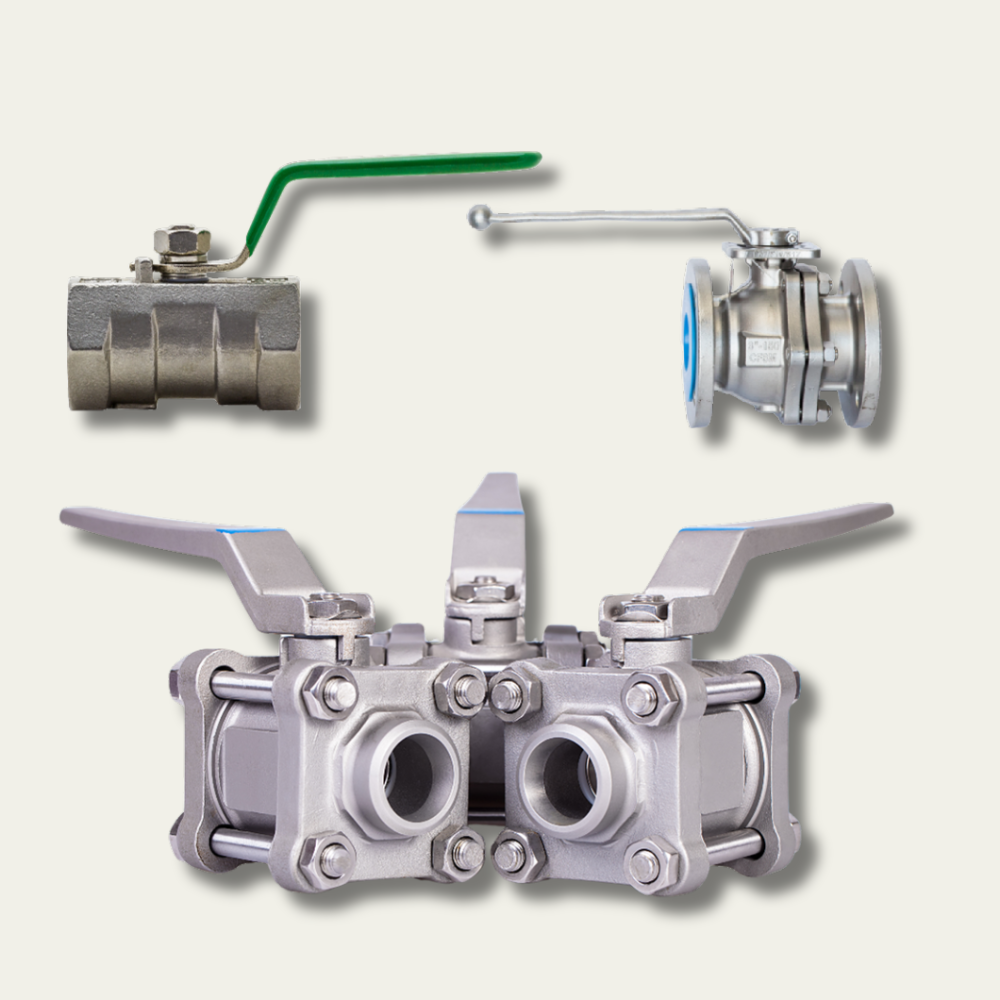
A ball valve is a quarter-turn isolation valve that uses a rotating ball with a bore through its centre to regulate flow. When the bore aligns with the pipeline, media flows freely. Rotating the ball ninety degrees shuts off the flow completely.
Ball valves are widely preferred because they offer:
- Fast operation
- Excellent sealing performance
- Low maintenance requirements
- Long service life
- Reliable shut-off capability
- Compatibility with manual and automated systems
Their simple operating mechanism makes them suitable for both routine operations and critical industrial processes where dependable isolation is essential.
Start by Evaluating Your Application
Every industrial process has unique operating conditions. Instead of choosing a valve solely based on pipe size or price, evaluate the complete operating environment.
Important factors include:
- Working pressure
- Operating temperature
- Type of media
- Flow rate
- Frequency of operation
- Required shut-off performance
- Installation location
- Automation requirements
For example, a valve handling potable water has very different requirements compared to one controlling abrasive slurry or corrosive chemicals.
At Flowlink Valves & Controls, our engineering team works closely with customers to recommend products that match both technical specifications and operational goals.
Understand the Different Ball Valve Designs
Choosing the correct valve design plays a significant role in overall system performance.
Floating Ball Valve
A floating ball valve supports the ball using two valve seats. During operation, upstream pressure pushes the ball against the downstream seat, creating a reliable seal.
Floating ball valves are commonly used for:
- Water distribution
- Chemical processing
- Food manufacturing
- General industrial services
- Utility applications
They are ideal for small to medium-sized pipelines where pressure ratings remain within standard operating limits.
Their simple construction also makes maintenance easier while keeping ownership costs relatively low.
Trunnion Ball Valve
For larger pipelines and high-pressure applications, a trunnion ball valve provides superior stability.
Unlike floating designs, the ball is mechanically supported by upper and lower trunnions, allowing operating torque to remain low even under high pressure.
These valves are frequently selected for:
- Oil and gas facilities
- Mining operations
- Power generation
- Pipeline transmission
- Petrochemical plants
Because the ball remains securely supported, sealing performance remains consistent while actuator sizing requirements are reduced.
Full Port or Reduced Port?
Another important consideration is valve bore size.
A full port ball valve has an internal bore equal to the pipeline diameter. This allows unrestricted flow while reducing pressure loss throughout the system.
Advantages include:
- Maximum flow capacity
- Lower pressure drop
- Improved pigging capability
- Reduced turbulence
- Better handling of slurries and viscous fluids
Reduced port valves, on the other hand, have a smaller internal opening. They are often selected where complete flow capacity is not essential and installation space or cost optimisation is a priority.
Understanding the process requirements helps determine which option delivers the best long-term value.
Match the Valve Material to the Process Media
Material selection is equally important when deciding how to choose a ball valve.
The wrong body or seat material can lead to corrosion, leakage, premature wear, and expensive downtime.
Common body materials include:
- Stainless steel
- Carbon steel
- Duplex stainless steel
- Cast steel
- Alloy materials
Seat materials vary depending on temperature and chemical compatibility and may include PTFE, reinforced PTFE, PEEK, metal seats, and other engineered materials.
The correct material combination depends on:
- Corrosive chemicals
- Steam
- Water
- Gas
- Hydrocarbons
- Abrasive media
- High-temperature applications
Selecting compatible materials significantly improves valve lifespan while reducing maintenance costs.
Pressure and Temperature Ratings Matter
Every valve is manufactured with specific pressure and temperature limitations.
Before making your selection, always verify:
- Maximum operating pressure
- Normal working pressure
- Peak pressure conditions
- Continuous operating temperature
- Maximum temperature excursions
Industrial systems frequently experience changing operating conditions. Choosing a valve with appropriate safety margins helps protect equipment while ensuring consistent performance.
Flowlink Valves & Controls supplies valves engineered to meet demanding Australian industrial environments, giving customers confidence that each valve is designed for reliable long-term operation.
Consider Industry Standards and Certifications
Industrial facilities often require compliance with recognised international standards.
For many critical applications, API ball valves are preferred because they are manufactured and tested according to recognised American Petroleum Institute standards.
API-certified valves offer greater confidence in:
- Product quality
- Pressure integrity
- Leak prevention
- Manufacturing consistency
- Operational safety
Depending on your project, additional standards such as AS, ISO, MSS, or fire-safe certifications may also be required.
Working with an experienced valve supplier helps ensure your selected products meet applicable project specifications and industry regulations.
Select the Right End Connection
The way a valve connects to your piping system is just as important as the valve itself. Selecting the correct end connection improves installation efficiency, minimises leakage risks, and simplifies future maintenance.
Common connection types include:
- Threaded ends for smaller piping systems and utility services.
- Flanged ends for medium and large industrial pipelines requiring secure connections.
- Butt weld ends for permanent installations where maximum strength is required.
- Socket weld ends for high-pressure piping with smaller diameters.
The best connection depends on your plant design, maintenance strategy, and operating conditions. Our team works with customers to recommend connection types that integrate seamlessly with existing systems while complying with Australian industry standards.
Consider Manual or Automated Operation
Modern industrial facilities increasingly rely on automation to improve productivity and operational safety.
While manual lever-operated valves remain suitable for many applications, automated ball valves provide greater control where frequent operation or remote monitoring is required.
Automation offers several advantages:
- Faster process control
- Reduced manual intervention
- Improved operator safety
- Better integration with plant control systems
- Consistent valve positioning
Depending on your process requirements, actuators may be pneumatic, electric, or hydraulic. Selecting the correct actuator ensures reliable valve performance while supporting efficient plant operations.
Think About Maintenance Before Installation
A quality valve should not only perform well today but also remain reliable for years to come.
When evaluating an industrial ball valve, consider its maintenance requirements throughout its service life.
Look for features such as:
- Replaceable seats
- Easy access to sealing components
- Serviceable stem assemblies
- High-quality sealing materials
- Durable corrosion-resistant construction
Although premium valves may involve a higher initial investment, they often reduce maintenance costs and minimise unexpected downtime over the long term.
Leakage Prevention Should Be a Priority
Industrial facilities cannot afford product loss, environmental contamination, or safety hazards caused by valve leakage.
Reliable sealing depends on multiple factors, including:
- Seat material
- Stem sealing design
- Manufacturing precision
- Pressure rating
- Installation quality
High-performance valves are designed to maintain tight shut-off performance even after repeated operation. Choosing products manufactured under strict quality control standards helps ensure long-term sealing reliability.
Fire-Safe Performance for Critical Applications
Some industries operate in environments where fire safety is a mandatory design requirement.
Oil and gas facilities, chemical processing plants, and energy infrastructure often require fire-safe ball valves capable of maintaining shut-off performance even after exposure to extreme temperatures.
Fire-safe valve designs typically include:
- Secondary metal-to-metal sealing
- Fire-tested construction
- High-temperature sealing materials
- Compliance with recognised international standards
When your application involves hazardous media, fire-safe certification should always be considered during the valve selection process.
Don’t Overlook Fugitive Emissions
Environmental compliance continues to become more important across Australian industries.
Valves handling gases or volatile chemicals should be designed to minimise fugitive emissions through advanced stem sealing systems.
High-quality sealing technology helps:
- Reduce product loss
- Improve workplace safety
- Support environmental compliance
- Lower operational costs
Choosing valves designed for emission control contributes to both regulatory compliance and sustainable operations.
Evaluate the Total Cost of Ownership
Many buyers focus primarily on purchase price, but long-term operating costs often have a much greater impact on overall project value.
A proper valve selection guide should consider:
- Installation costs
- Maintenance frequency
- Downtime risks
- Replacement intervals
- Energy efficiency
- Spare parts availability
A well-engineered valve with a longer service life frequently delivers greater value than a lower-cost alternative requiring frequent repairs or replacement.
At Flowlink Valves & Controls, we help customers evaluate the complete lifecycle of their valve investment rather than focusing solely on upfront cost.
Common Mistakes When Choosing a Ball Valve
Even experienced buyers occasionally overlook important technical details. Avoiding these common mistakes can improve system reliability and reduce maintenance issues.
One of the most common errors is selecting a valve based only on pipe size. While size is important, pressure, temperature, media characteristics, and operating frequency must also be considered.
Another mistake is choosing materials without evaluating chemical compatibility. Corrosion and seal degradation can significantly shorten valve life.
Many facilities also underestimate future maintenance requirements. Selecting serviceable valves with readily available replacement parts can simplify long-term maintenance planning.
Ignoring applicable industry standards is another issue. Projects requiring API ball valves or other certified products should always specify compliant equipment during procurement.
Finally, purchasing solely on price rather than performance often leads to increased operating costs over time.
Ball Valve Applications Across Australian Industries
Ball valves play a vital role across numerous industrial sectors throughout Australia.
Mining
Mining operations require robust valves capable of handling abrasive media, high pressures, and demanding operating environments.
Water and Wastewater
Reliable shut-off valves help maintain efficient treatment processes while supporting long-term infrastructure performance.
Oil and Gas
Critical process isolation demands durable valves with dependable sealing performance and compliance with recognised industry standards.
Chemical Processing
Chemical plants rely on corrosion-resistant materials and precise sealing systems to safely handle aggressive process media.
Manufacturing
Production facilities benefit from valves that deliver reliable operation while reducing maintenance interruptions and improving productivity.
Energy and Utilities
Power generation facilities require dependable flow control solutions capable of operating under varying pressures and temperatures.
Our extensive product portfolio enables us to support customers across these industries with solutions designed for performance, safety, and reliability.
Engineering Support Makes the Difference
Choosing the right valve is not simply about selecting a catalogue product. Every application presents unique challenges that require technical understanding and practical experience.
At Flowlink Valves & Controls, we assist customers throughout the selection process by evaluating operating conditions, application requirements, compliance needs, and long-term maintenance considerations.
Our objective is to supply valve solutions that provide dependable performance while helping customers improve operational efficiency and reduce lifecycle costs.
Why Choose Flowlink Valves & Controls?
Selecting the right valve supplier is just as important as choosing the correct valve. A trusted supplier provides more than products. They offer technical expertise, dependable support, and solutions tailored to your operational requirements.
At Flowlink Valves & Controls, we are committed to delivering high-quality industrial valve solutions for customers across Australia. Our extensive product range, engineering knowledge, and focus on quality allow us to support projects of every scale, from routine maintenance to complex industrial installations.
Whether you require a floating ball valve, trunnion ball valve, full port ball valve, or other specialised valve solutions, our team works closely with you to recommend products that align with your operating conditions, industry standards, and long-term performance goals.
By combining quality products with expert technical support, we help businesses improve system reliability, reduce maintenance requirements, and maximise operational efficiency.
Conclusion
Understanding how to choose a ball valve involves much more than selecting a valve that fits the pipeline. Factors such as operating pressure, temperature, process media, valve design, material selection, certification requirements, and automation all contribute to long-term performance and reliability.
Taking a structured approach to valve selection helps reduce downtime, improve plant efficiency, and protect your investment for years to come.
At Flowlink Valves & Controls, we provide dependable valve solutions backed by industry expertise and technical support. Whether your application requires standard isolation valves or specialised API ball valves for demanding industrial environments, our experienced team is ready to help you choose the right solution with confidence.
Frequently Asked Questions
1. How do I choose the right ball valve for my industrial application?
The right ball valve depends on factors such as operating pressure, temperature, media type, pipe size, and industry requirements. Evaluating these conditions ensures reliable performance and a longer service life.
2. What is the difference between a floating ball valve and a trunnion ball valve?
A floating ball valve relies on line pressure to create a seal and is commonly used in smaller systems. A trunnion ball valve uses mechanical supports for the ball, making it suitable for high-pressure and large-diameter industrial applications.
3. When should I use a full port ball valve?
A full port ball valve is ideal when maintaining maximum flow capacity is important. It reduces pressure loss, supports efficient flow, and is commonly used in pipelines handling liquids, slurries, and process fluids.
4. Why are API ball valves important for industrial projects?
API ball valves are manufactured and tested according to recognised industry standards, helping ensure quality, safety, and reliable performance in demanding applications such as oil and gas, petrochemical processing, and energy production.
5. Can Flowlink Valves & Controls help me select the right valve?
Yes. Our experienced team evaluates your operating conditions, application requirements, and industry standards to recommend the most suitable valve solution for your project, helping improve efficiency and long-term reliability.