Flowlink Valves & Controls

Blog

Industrial Valves for Oil & Gas

Essential Industrial Valves Used in Oil & Gas Applications

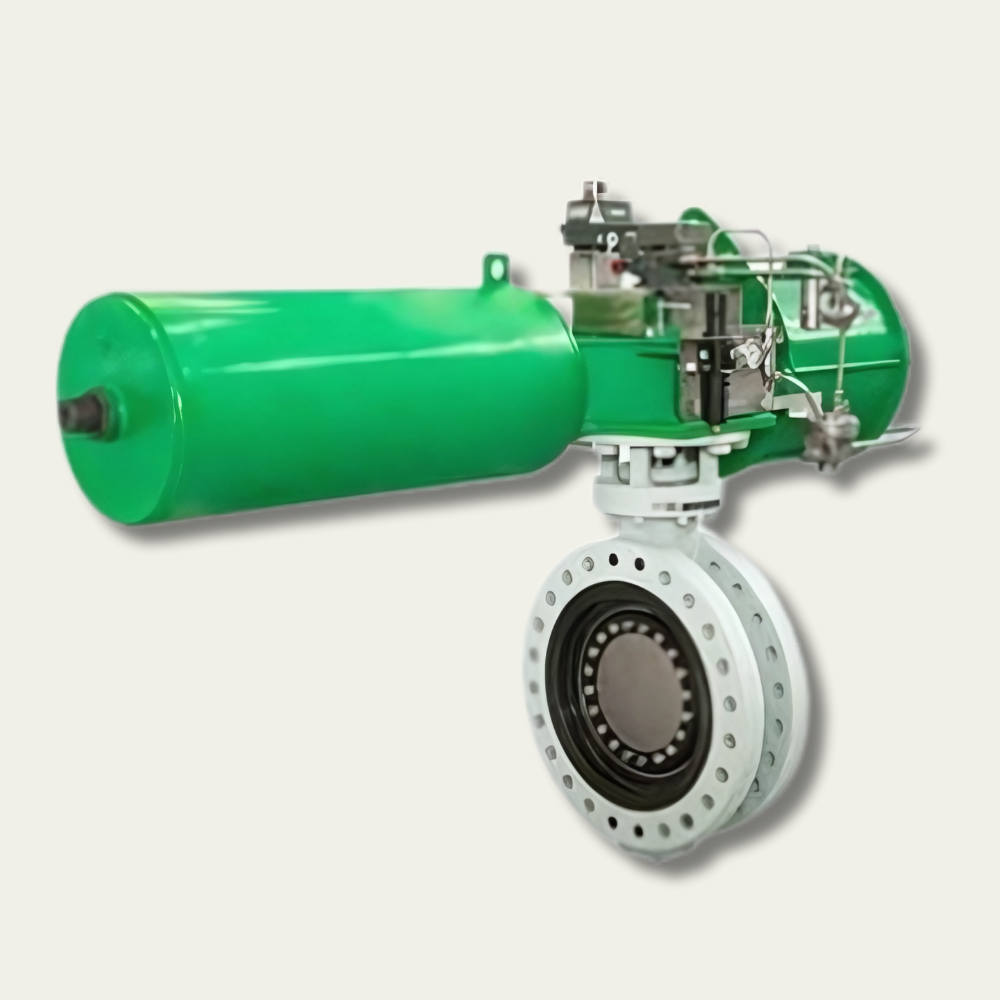
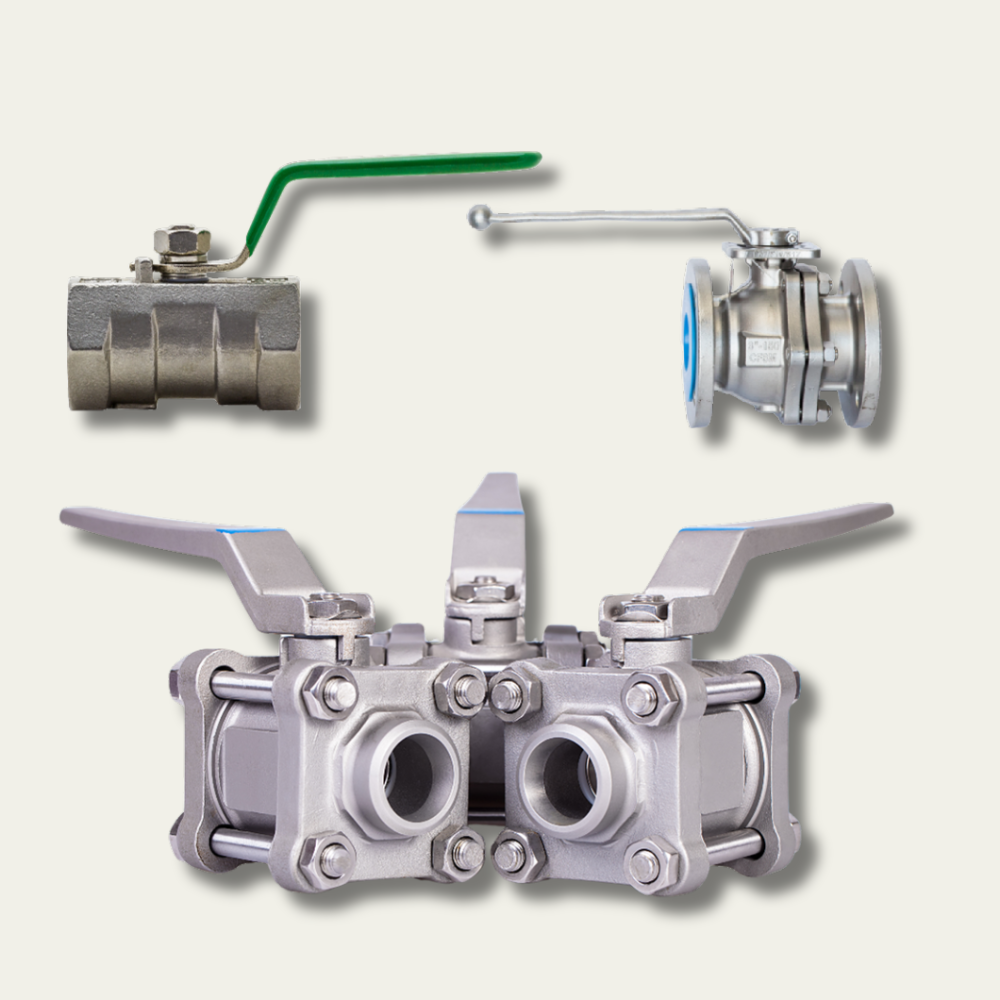
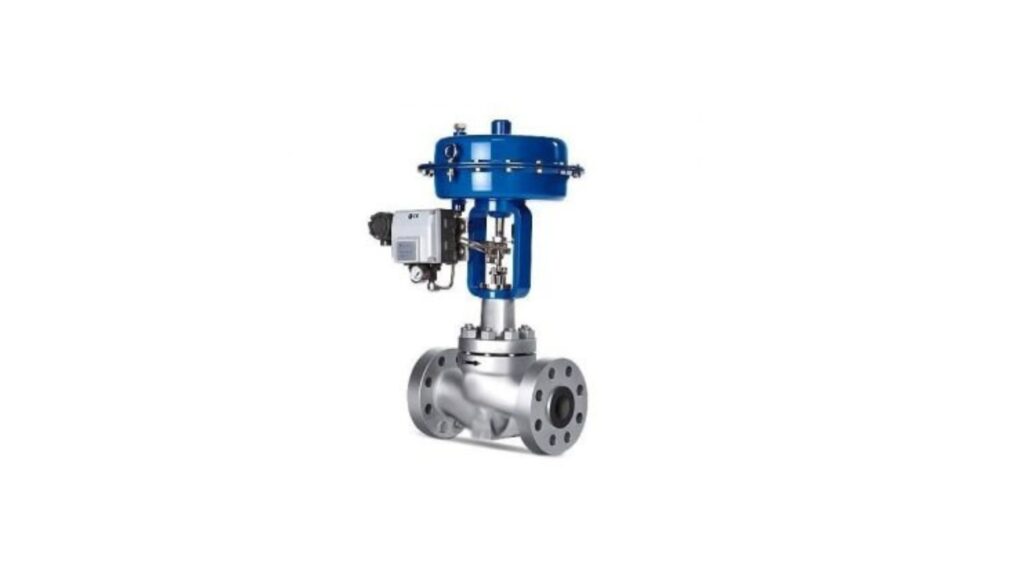
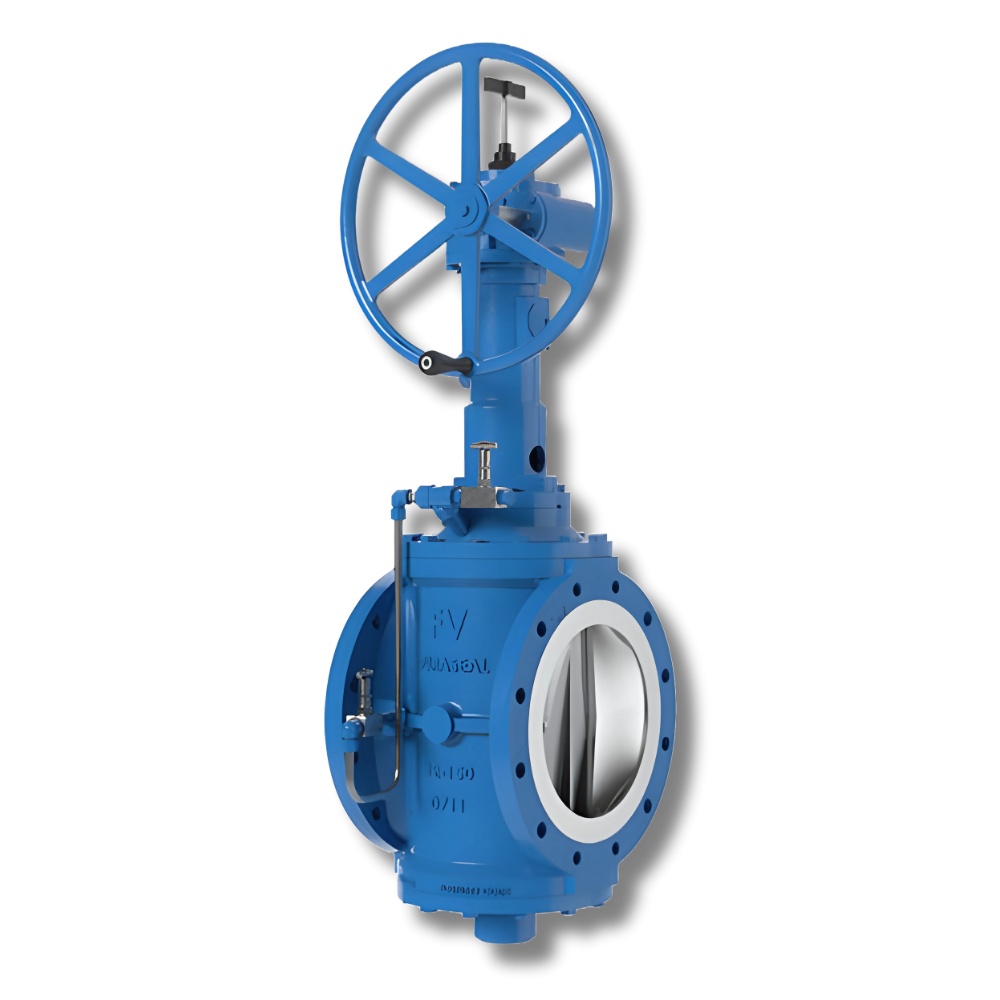
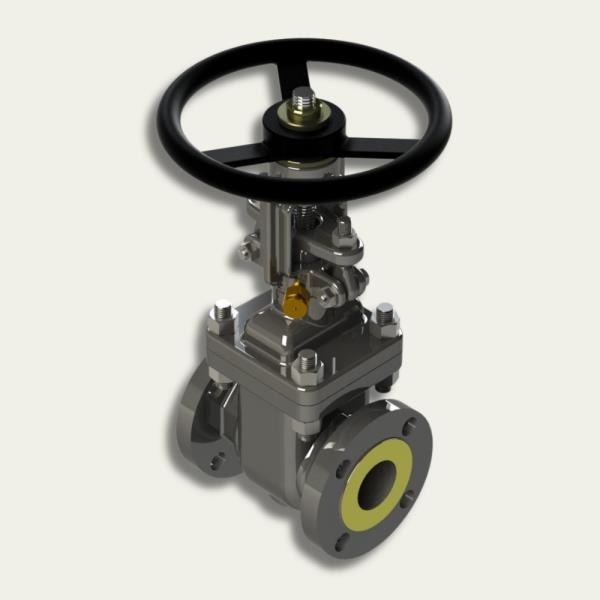
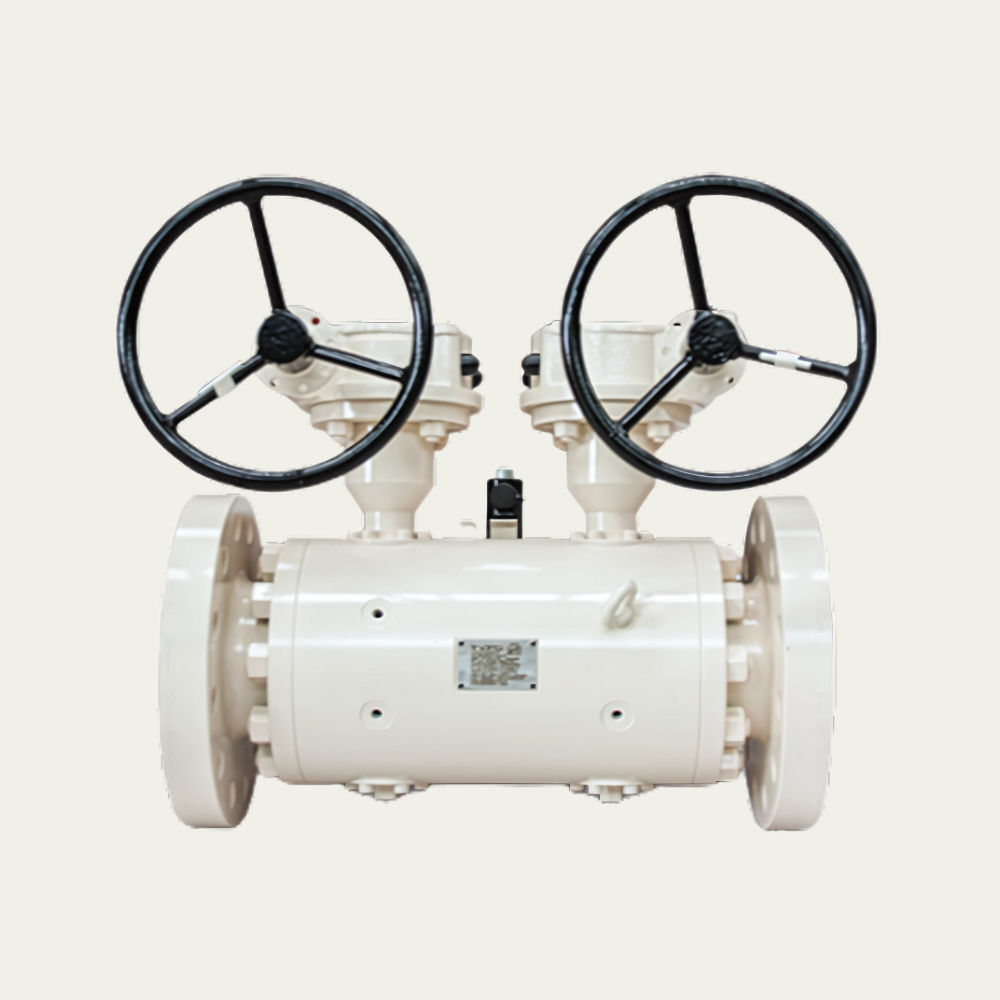
The oil and gas industry operates under demanding conditions where high pressure, extreme temperatures, corrosive fluids, flammable materials, and continuous flow are common. In such environments, reliable industrial valves for oil and gas are essential for controlling, isolating, regulating, and directing the movement of liquids and gases throughout production and processing systems. From exploration and wellhead operations to pipelines, storage facilities, refineries, and LNG plants, the right valve plays a critical role in maintaining safety, efficiency, and operational continuity. Oil and gas facilities require valves that can deliver dependable performance while meeting strict engineering and safety requirements. Flowlink Valves & Controls provides integrated valve, actuation, control, and flow equipment solutions for the oil and gas sector, supporting upstream, midstream, and downstream applications across Australia and the wider region. Flowlink Valves & Controls oil and gas solutions Why Industrial Valves Are Important in Oil & Gas Valves are among the most important mechanical components within an oil and gas facility. Their primary purpose is to control the movement of oil, gas, water, chemicals, and other process fluids. However, their role goes far beyond simple flow control. A properly selected valve can help operators isolate equipment during maintenance, prevent unwanted backflow, regulate process conditions, minimise leakage, and protect critical assets from excessive pressure. Valve reliability is particularly important in oil and gas applications because valve failure can lead to production interruptions, environmental incidents, equipment damage, or serious safety risks. The selection process should consider factors such as operating pressure, temperature, fluid characteristics, pipe size, flow requirements, corrosion potential, emission requirements, maintenance needs, and applicable industry standards. 1. Ball Valves Ball valves are widely used throughout oil and gas facilities because they provide reliable shutoff and quick operation. Their design uses a rotating ball with a central opening to control flow. When the valve is fully open, the bore provides a relatively unrestricted flow path, while rotating the ball 90 degrees closes the valve. Ball valves are commonly used in pipelines, wellhead systems, gas processing facilities, storage systems, terminals, and refinery applications. Trunnion-mounted ball valves are particularly suitable for demanding high-pressure applications. They can incorporate features such as double block and bleed capability, cavity relief, emergency sealant injection, fire-safe construction, and fugitive emission control. Flowlink’s trunnion-mounted ball valve range includes designs compliant with standards such as API 6D, API 608, ISO 17292, and ASME B16.34. Their major advantages include: For critical isolation applications, selecting the appropriate ball valve design is essential for achieving dependable long-term performance. 2. Gate Valves Gate valves are commonly used when full flow or complete isolation is required. Instead of regulating flow through a partially open position, a gate valve is generally designed to operate in either a fully open or fully closed position. This makes gate valves suitable for applications where maintaining a low pressure drop through the pipeline is important. They are frequently used in transmission pipelines, oil and gas processing facilities, storage systems, and other applications where reliable isolation is required. Gate valves are available in different configurations and materials to accommodate various pressure, temperature, and fluid conditions. When used correctly, they can provide robust isolation and long service life. However, gate valves are generally not the first choice for continuous throttling because partially opening the valve can result in undesirable flow characteristics and increased wear. 3. Globe Valves Globe valves are designed primarily for flow regulation and throttling. Their internal configuration allows operators to adjust the flow rate with greater precision than many isolation valve designs. In oil and gas facilities, globe valves may be used in process control systems, pressure regulation applications, bypass systems, and other services where accurate flow adjustment is required. Because throttling can generate pressure losses, globe valves need to be selected according to the specific process conditions. Correct sizing is particularly important because an incorrectly sized valve can negatively affect control accuracy, energy efficiency, and equipment performance. For automated applications, globe valves can also be integrated with suitable actuation and control systems. 4. Check Valves Check valves are designed to allow fluid to flow in one direction while preventing reverse flow. They are particularly important in oil and gas systems because unwanted backflow can damage pumps, compressors, pipelines, and other equipment. Depending on the application, different check valve designs can be used, including swing, piston, lift, and other specialised configurations. Check valves can be installed in pipeline systems, pump discharge lines, compressor systems, process units, and other locations where reverse flow must be controlled. Selecting the correct check valve requires consideration of flow velocity, pressure, temperature, fluid properties, installation position, and potential pressure surge. 5. Butterfly Valves Butterfly valves use a rotating disc to control flow and are often selected when compact construction, lower weight, and efficient operation are important. They can be used in a variety of oil and gas applications, particularly in larger diameter piping systems. Depending on the design, butterfly valves can provide effective isolation and flow control while requiring less space than some larger valve types. The selection of seat material, body material, pressure class, actuator, and disc design is important when using butterfly valves in demanding environments. For automated systems, pneumatic or electric actuation can be added to enable remote operation and integration with plant control systems. 6. DBB Valves DBB valves, or Double Block and Bleed valves, are particularly important in applications where positive isolation is required. A DBB arrangement provides two independent sealing barriers with a bleed or vent point between them. This configuration can help operators verify isolation and safely release trapped pressure from the cavity between the barriers. DBB valves can therefore be valuable in applications involving maintenance, equipment isolation, hazardous fluids, and critical process systems. They are commonly considered for pipeline systems, terminals, storage facilities, refinery applications, metering systems, and other areas where enhanced isolation is required. Flowlink provides DBB valves and SBB DBB solutions as part of its oil and gas valve portfolio. 7. API Valves The term API valves generally refers to valves designed, manufactured, tested, or
Pressure Safety Valve vs Pressure Relief Valve

Pressure Safety Valve vs Pressure Relief Valve: What’s the Difference?

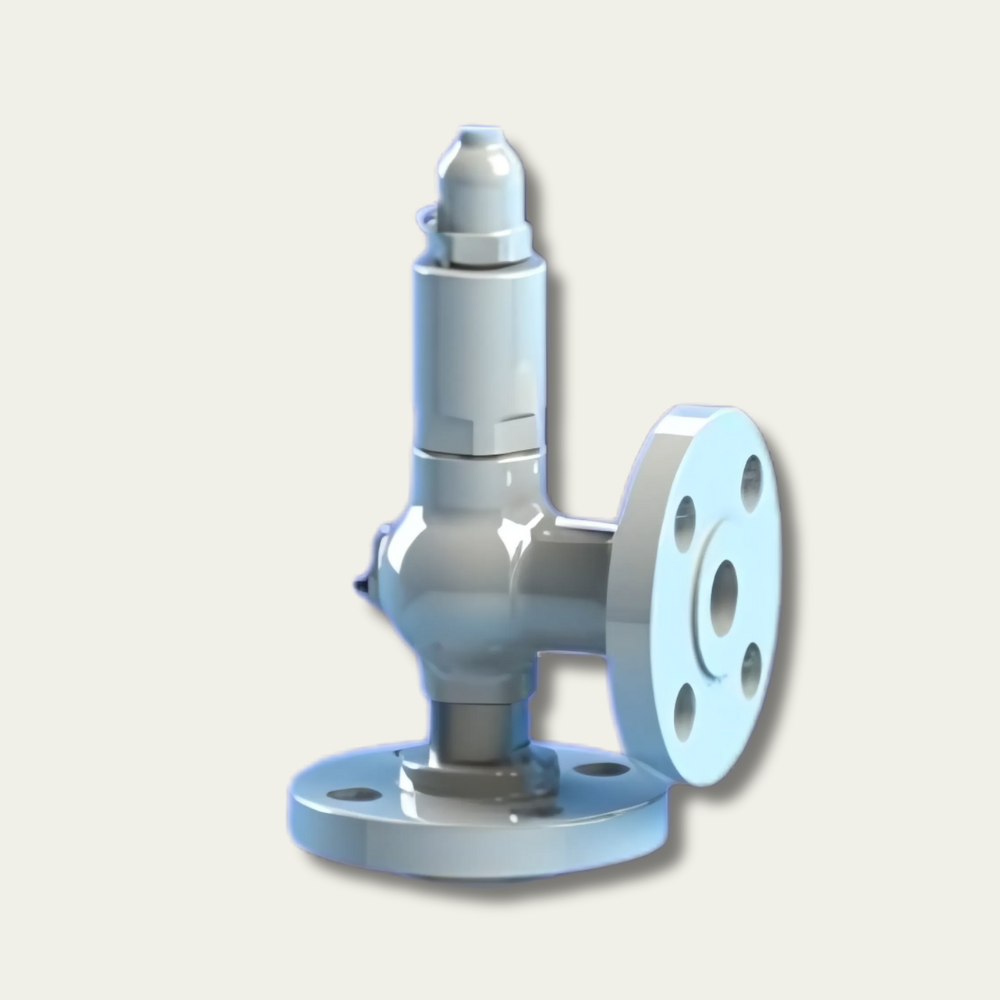
When comparing a pressure safety valve vs. pressure relief valve, it is important to understand that both devices are designed to protect pressurised systems from potentially dangerous pressure conditions. Still, their applications, operating characteristics, and terminology can differ. In industrial facilities, selecting the correct pressure protection device is essential for protecting equipment, maintaining process reliability, and supporting safe plant operation. Understanding the difference between a Pressure Safety Valve (PSV) and a Pressure Relief Valve (PRV) can help engineers and plant operators make better decisions for oil and gas, mining, petrochemical, power generation, water, and other demanding applications. What Is a Pressure Safety Valve? A Pressure Safety Valve, commonly known as a PSV, is a safety device that automatically releases excess pressure when system pressure reaches a predetermined set point. PSVs are particularly associated with applications involving compressible fluids such as gases and steam. When system pressure rises beyond the defined limit, the valve opens rapidly to discharge the excess pressure. Once the pressure returns to a safe level, the valve closes according to its design characteristics. The primary purpose of a PSV is not normal pressure control. Instead, it acts as a protective device during abnormal or emergency conditions. For example, a steam system may experience excessive pressure because of a blocked outlet, equipment malfunction, fire exposure, or failure of a control system. A properly sized PSV can provide a final layer of protection by relieving pressure before the equipment exceeds its allowable design limits. Flowlink Valves & Controls provides engineered pressure safety solutions for demanding industrial applications. Its product range includes pressure safety valves designed for different pressure, temperature, material, and service requirements. Flowlink’s documented valve range includes designs aligned with standards such as API 520, API 521, API 526, and API 527. What Is a Pressure Relief Valve? A Pressure Relief Valve, or PRV, is another type of pressure protection device used to prevent excessive pressure from damaging equipment and piping systems. The term PRV can be used broadly across different industries, and its exact meaning can vary depending on the application and engineering convention. In many industrial contexts, a pressure relief valve is associated with liquid service and is designed to open when pressure exceeds a predetermined set pressure. Unlike a conventional control valve, a PRV is primarily intended to protect the system from abnormal pressure conditions rather than continuously regulate process pressure. For example, a liquid-filled pipeline can experience thermal expansion when a blocked-in liquid is exposed to rising temperatures. Even a relatively small amount of thermal expansion can create a significant increase in pressure. A properly selected relief valve can discharge the excess fluid and prevent the pressure from exceeding the allowable limit. Flowlink offers a range of pressure regulating and relieving solutions, including pressure relieving and reducing valves, direct-acting pressure regulators, pilot-operated self-actuated pressure regulators, and slam shut-off valves. PSV vs PRV: What Is the Main Difference? The simplest way to understand PSV vs PRV is to consider the type of service, operating characteristics, and terminology used for the valve. A PSV is generally associated with protection against excessive pressure in systems containing gases or vapours and is commonly designed for rapid opening when the set pressure is reached. A PRV is often associated with liquid applications, where the valve opens progressively to relieve excessive pressure. However, terminology is not always consistent across industries. Some manufacturers, engineers, standards, and regions may use PRV as a general term for pressure-relieving devices, while others distinguish between PSV and PRV based on fluid service and valve operating characteristics. Therefore, engineers should not select a valve based only on whether it is labelled PSV or PRV. The actual application, fluid characteristics, pressure conditions, temperature, required capacity, applicable standards, and equipment design pressure must all be evaluated. Key Differences Between Pressure Safety Valve and Pressure Relief Valve 1. Typical Fluid Service One of the most common distinctions is the type of fluid being handled. PSVs are frequently used for gases, vapours, and steam applications. PRVs are often associated with liquids. However, this is not an absolute rule. The appropriate device depends on the engineering requirements of the specific application. 2. Opening Characteristics A PSV used in gas or vapour service may be designed to open rapidly once the set pressure is reached. Rapid opening allows the valve to release pressure quickly during an abnormal event. A relief valve used for liquid service may open progressively as pressure increases. This characteristic is useful when controlling pressure in liquid systems where sudden discharge could create undesirable process conditions. 3. Primary Purpose Both devices provide pressure protection, but they should not be confused with ordinary pressure control valves. A pressure control valve continuously adjusts flow to maintain a desired operating condition. A safety or relief valve generally remains closed during normal operation and activates when pressure reaches its specified set point. This distinction is critical because pressure protection devices should not normally be used as substitutes for continuous process control. 4. Application Environment PSVs are widely used in applications such as steam systems, gas processing, pressure vessels, refineries, petrochemical plants, and other systems where compressible fluids may create dangerous overpressure conditions. PRVs can be used in liquid systems such as pipelines, hydraulic systems, chemical processing equipment, and liquid storage or transfer applications. The selection must always be based on the complete process design rather than simply the industry name. Why Pressure Protection Is Essential in Industrial Systems Pressure protection is one of the most important elements of industrial process safety. Industrial systems can experience unexpected pressure increases for many reasons, including: Without adequate pressure protection, excessive pressure can damage vessels, pipelines, pumps, heat exchangers, compressors, and other critical equipment. In severe cases, overpressure can result in equipment rupture, release of hazardous substances, fire, environmental damage, or serious injury. This is why pressure safety devices need to be correctly specified, sized, installed, tested, and maintained. Understanding API Safety Valves API safety valves are particularly important in industries where recognised engineering standards and

Check Valve Failure

Check Valve Failure: Common Causes, Warning Signs and Prevention Tips for Reliable System Performance

A properly functioning check valve plays a vital role in maintaining safe and efficient fluid flow across industrial systems. Understanding the reasons behind check valve failure is essential for preventing equipment damage, reducing maintenance costs, and ensuring uninterrupted operations. Whether used in water treatment, mining, oil and gas, chemical processing, or manufacturing, check valves are designed to allow fluid to flow in one direction while preventing reverse flow. At our company, we supply high-quality industrial valve solutions engineered for demanding operating conditions. Our range includes swing check valve and dual plate check valve options that provide dependable backflow prevention and long-term performance across various industries. By identifying the common causes of valve failure and following proper maintenance practices, businesses can improve system reliability and extend the lifespan of their equipment. This guide explains why check valves fail, how to recognize early warning signs, and the best preventive measures to keep your systems operating efficiently. Why Check Valves Are Essential in Industrial Systems Check valves perform a simple yet critical function by automatically preventing reverse flow. Unlike manually operated valves, they work without external control, opening when forward pressure is sufficient and closing when flow reverses. Without a reliable check valve, reverse flow can cause serious operational issues, including equipment damage, contamination, pressure fluctuations, and costly downtime. Common applications include: Selecting the correct industrial check valve helps protect pumps, compressors, pipelines, and other valuable equipment. What Is Check Valve Failure? Check valve failure occurs when the valve no longer performs its primary function of preventing reverse flow or regulating directional movement of fluids. Failure may develop gradually due to wear or appear suddenly because of improper installation, pressure surges, or unsuitable operating conditions. In many cases, valve failure affects the efficiency of the entire piping system, leading to higher maintenance costs and unexpected shutdowns. Recognizing the root causes allows maintenance teams to address problems before they become major operational issues. Common Causes of Check Valve Failure Understanding why failures occur is the first step toward improving system reliability. 1. Incorrect Valve Selection One of the most common reasons for premature failure is choosing the wrong valve for the application. Several factors must be evaluated before installation, including: Using an unsuitable valve can result in excessive wear, poor sealing performance, or repeated operational failures. 2. Poor Installation Practices Even a high-quality valve can underperform if installed incorrectly. Common installation mistakes include: Carefully following installation guidelines helps ensure the valve functions as intended from the first day of operation. 3. Water Hammer and Pressure Surges Rapid pressure changes place tremendous stress on internal valve components. Water hammer occurs when fluid flow stops suddenly, creating a shock wave throughout the piping system. Repeated pressure surges may cause: Selecting the appropriate valve design and maintaining stable system pressure significantly reduces these risks. 4. Wear and Tear from Continuous Operation Industrial systems often operate around the clock. Over time, continuous cycling naturally causes wear on moving parts. Components that commonly experience wear include: Routine inspections help identify wear before it affects valve performance. 5. Corrosion and Chemical Exposure Harsh operating environments accelerate valve deterioration. Corrosion may result from: Choosing corrosion-resistant materials for demanding applications greatly improves service life and reduces maintenance requirements. Warning Signs That a Check Valve May Be Failing Early detection prevents costly equipment damage and unplanned downtime. Some common warning signs include: When any of these symptoms appear, the valve should be inspected as soon as possible to determine the underlying cause. Understanding Different Types of Check Valves Selecting the right valve design is an important part of preventing premature failures. Swing Check Valve A swing check valve uses a hinged disc that opens with forward flow and closes automatically when flow reverses. Its advantages include: Swing check valves are commonly used in water distribution systems, pumping stations, and industrial processing facilities where unrestricted flow is important. Dual Plate Check Valve A dual plate check valve features two spring-loaded plates that open with forward flow and close rapidly when the flow stops. This design provides several advantages: Dual plate check valves are widely used in high-pressure industrial systems where quick response and efficient backflow prevention are essential. Selecting the Right Industrial Check Valve Choosing the correct industrial check valve is one of the most effective ways to reduce the risk of premature failure. Every application has different operating conditions, so the valve should always be selected based on the actual system requirements rather than price alone. Important selection factors include: A properly selected valve delivers better sealing performance, longer service life, and improved operational efficiency. The Importance of Backflow Prevention One of the primary purposes of a check valve is backflow prevention. Reverse flow can damage pumps, contaminate clean water systems, and create unstable pressure conditions throughout the pipeline. Effective backflow prevention offers several benefits: Selecting a high-quality check valve with dependable sealing characteristics helps maintain uninterrupted operations while protecting valuable equipment. How Valve Maintenance Prevents Failure Preventive valve maintenance plays a major role in extending the lifespan of check valves. Regular inspections allow maintenance teams to identify wear before it develops into a larger issue. A routine maintenance schedule should include: Keeping maintenance records also helps identify recurring issues and supports better long-term planning. Common Installation Mistakes to Avoid Incorrect installation is one of the leading causes of early valve failure. Following manufacturer recommendations helps ensure reliable operation from the beginning. Avoid these common mistakes: Proper installation minimizes unnecessary stress on the valve and improves sealing performance. Material Selection Matters The material used in a check valve has a significant impact on durability and long-term reliability. Material selection should be based on: For demanding industrial environments, corrosion-resistant materials help reduce maintenance costs and improve service life. Selecting the appropriate body, disc, and sealing materials ensures the valve performs consistently under challenging operating conditions. Applications That Demand Reliable Check Valves Check valves are used across a wide range of industries where uninterrupted flow control is critical. Our valve solutions support applications such

butterfly valve

Butterfly Valve Selection Guide: Choosing the Right Butterfly Valve for Water, Mining and Industrial Systems

Selecting the right valve is one of the most important decisions when designing or upgrading any fluid handling system. A well-planned butterfly valve selection guide helps engineers, contractors, plant managers, and procurement teams choose a valve that delivers reliable flow control, long service life, and minimal maintenance. At our company, we manufacture and supply high-performance butterfly valves designed to meet the demanding requirements of water treatment facilities, mining operations, manufacturing plants, chemical processing systems, and other industrial applications. Whether you need a resilient butterfly valve, lug butterfly valve, wafer butterfly valve, or butterfly valve stainless model, selecting the correct product begins with understanding your operating conditions and performance expectations. This guide explains the key factors that influence butterfly valve selection, helping you make informed decisions that improve efficiency, reduce downtime, and maximize the value of your investment. Why Butterfly Valves Are Widely Used Butterfly valves have become one of the most popular valve types because they combine simple operation with reliable shut-off and flow regulation. Their compact design requires less installation space than many other valve types while offering excellent performance across a wide range of applications. Compared to larger gate or globe valves, butterfly valves are lighter, easier to install, and often more economical without sacrificing operational reliability. Industries commonly using butterfly valves include: Their versatility makes them suitable for both isolation and throttling applications. Understanding Your Application First Every system has unique operating conditions. Before choosing any valve, it is important to evaluate how the system will perform during daily operation. Questions to consider include: Answering these questions provides the foundation for selecting the most appropriate industrial butterfly valve. Selecting the Correct Butterfly Valve Type Different butterfly valve designs serve different installation requirements. Understanding these differences helps ensure optimal performance. Wafer Butterfly Valve A wafer butterfly valve is designed to fit between two pipeline flanges. It is one of the most economical and compact valve designs available. Benefits include: Wafer valves are commonly installed where bi-directional sealing is acceptable and piping loads remain moderate. Lug Butterfly Valve A lug butterfly valve features threaded inserts that allow the valve to be bolted directly between pipeline flanges. This design offers several advantages: Lug valves are frequently selected for mining plants, industrial processing facilities, and critical water distribution systems. Resilient Butterfly Valve A resilient butterfly valve incorporates an elastomer seat that creates a reliable bubble-tight seal. Advantages include: Municipal water treatment plants and distribution networks often prefer resilient seated butterfly valves because they offer dependable performance with minimal maintenance. Choosing the Right Valve Material Material selection directly impacts valve durability, corrosion resistance, and operational life. Common materials include cast iron, ductile iron, carbon steel, stainless steel, bronze, and specialty alloys. The correct material depends on: A valve installed in a drinking water system may require different materials than one handling mining slurry or corrosive chemicals. When to Choose Butterfly Valve Stainless Models For demanding industrial environments, butterfly valve stainless options provide superior resistance to corrosion and wear. Stainless steel valves are commonly selected for: Although stainless steel valves may involve a higher initial investment, they often deliver lower lifecycle costs due to reduced maintenance and longer operational life. Valve Sizing Matters More Than Many Realize Proper valve sizing is one of the most overlooked aspects of system design. An oversized valve can reduce flow control accuracy, while an undersized valve may increase pressure loss and reduce system efficiency. Several factors influence sizing: Selecting the correct valve size helps improve energy efficiency while extending the service life of pumps, actuators, and the valve itself. Pressure and Temperature Ratings Every butterfly valve is manufactured to operate within specified pressure and temperature limits. Before installation, verify that the valve rating matches your operating conditions. Consider: Choosing a valve with the proper rating improves safety and prevents premature equipment failure. Selecting the Right Disc and Seat Combination The interaction between the disc and seat determines sealing performance, wear resistance, and valve lifespan. Common seat materials include: Each material offers different advantages depending on the fluid and operating temperature. Similarly, disc materials should be selected based on corrosion resistance, strength, and compatibility with the process media. Selecting the Best Actuation Method The performance of a butterfly valve is influenced not only by its construction but also by the way it is operated. Choosing the correct actuation method improves efficiency, simplifies operation, and supports long-term system reliability. The three most common operating methods include manual, electric, and pneumatic actuation. Manual Operation Manual butterfly valves are commonly operated using a hand lever or gear operator. They are suitable for systems where valves are adjusted occasionally and where automation is not required. Typical applications include: Manual valves offer a practical and cost-effective solution for many installations while requiring minimal maintenance. Electric Actuation Electric actuators allow valves to be opened or closed remotely through automated control systems. They are widely used where precision, monitoring, and process integration are priorities. Electric actuated valves are ideal for: They can also be integrated with SCADA or PLC systems to improve operational efficiency and reduce manual intervention. Pneumatic Actuation Pneumatic butterfly valves use compressed air to provide fast and reliable operation. They are preferred in facilities where rapid cycling and dependable automation are essential. Common applications include: Their quick response and durability make them suitable for demanding industrial environments. Factors That Influence Valve Performance Selecting the right butterfly valve involves more than matching the pipe size. Several operating conditions directly affect performance and service life. Fluid Characteristics Different fluids place different demands on valve components. For example: Understanding the fluid being handled is one of the first steps in making the right valve selection. Operating Frequency Some valves remain open for long periods, while others cycle hundreds of times each day. High-cycle applications require: Selecting a valve designed for frequent operation reduces maintenance costs over time. Installation Environment Environmental conditions should also be evaluated before selecting a valve. Consider factors such as: Choosing suitable coatings and materials helps protect the valve throughout its

Ball Valve

How to Choose a Ball Valve for Industrial Applications in Australia 

Selecting the right valve is one of the most important decisions when designing or maintaining an industrial piping system. If you are wondering how to choose a ball valve, the answer depends on several technical and operational factors including pressure, temperature, media compatibility, installation environment, and maintenance expectations. Choosing the correct valve helps improve operational efficiency, reduce downtime, and extend equipment life. At Flowlink Valves & Controls, we supply high-quality valve solutions for a wide range of Australian industries. Our extensive product range is designed to meet demanding industrial requirements while delivering dependable performance in critical applications. Whether you require an industrial ball valve for water treatment, mining, manufacturing, oil and gas, chemical processing, or other industrial sectors, selecting the right valve begins with understanding your operating conditions. This guide explains the key considerations involved in selecting the right ball valve while helping you make an informed investment for long-term reliability. Understanding the Purpose of a Ball Valve A ball valve is a quarter-turn isolation valve that uses a rotating ball with a bore through its centre to regulate flow. When the bore aligns with the pipeline, media flows freely. Rotating the ball ninety degrees shuts off the flow completely. Ball valves are widely preferred because they offer: Their simple operating mechanism makes them suitable for both routine operations and critical industrial processes where dependable isolation is essential. Start by Evaluating Your Application Every industrial process has unique operating conditions. Instead of choosing a valve solely based on pipe size or price, evaluate the complete operating environment. Important factors include: For example, a valve handling potable water has very different requirements compared to one controlling abrasive slurry or corrosive chemicals. At Flowlink Valves & Controls, our engineering team works closely with customers to recommend products that match both technical specifications and operational goals. Understand the Different Ball Valve Designs Choosing the correct valve design plays a significant role in overall system performance. Floating Ball Valve A floating ball valve supports the ball using two valve seats. During operation, upstream pressure pushes the ball against the downstream seat, creating a reliable seal. Floating ball valves are commonly used for: They are ideal for small to medium-sized pipelines where pressure ratings remain within standard operating limits. Their simple construction also makes maintenance easier while keeping ownership costs relatively low. Trunnion Ball Valve For larger pipelines and high-pressure applications, a trunnion ball valve provides superior stability. Unlike floating designs, the ball is mechanically supported by upper and lower trunnions, allowing operating torque to remain low even under high pressure. These valves are frequently selected for: Because the ball remains securely supported, sealing performance remains consistent while actuator sizing requirements are reduced. Full Port or Reduced Port? Another important consideration is valve bore size. A full port ball valve has an internal bore equal to the pipeline diameter. This allows unrestricted flow while reducing pressure loss throughout the system. Advantages include: Reduced port valves, on the other hand, have a smaller internal opening. They are often selected where complete flow capacity is not essential and installation space or cost optimisation is a priority. Understanding the process requirements helps determine which option delivers the best long-term value. Match the Valve Material to the Process Media Material selection is equally important when deciding how to choose a ball valve. The wrong body or seat material can lead to corrosion, leakage, premature wear, and expensive downtime. Common body materials include: Seat materials vary depending on temperature and chemical compatibility and may include PTFE, reinforced PTFE, PEEK, metal seats, and other engineered materials. The correct material combination depends on: Selecting compatible materials significantly improves valve lifespan while reducing maintenance costs. Pressure and Temperature Ratings Matter Every valve is manufactured with specific pressure and temperature limitations. Before making your selection, always verify: Industrial systems frequently experience changing operating conditions. Choosing a valve with appropriate safety margins helps protect equipment while ensuring consistent performance. Flowlink Valves & Controls supplies valves engineered to meet demanding Australian industrial environments, giving customers confidence that each valve is designed for reliable long-term operation. Consider Industry Standards and Certifications Industrial facilities often require compliance with recognised international standards. For many critical applications, API ball valves are preferred because they are manufactured and tested according to recognised American Petroleum Institute standards. API-certified valves offer greater confidence in: Depending on your project, additional standards such as AS, ISO, MSS, or fire-safe certifications may also be required. Working with an experienced valve supplier helps ensure your selected products meet applicable project specifications and industry regulations. Select the Right End Connection The way a valve connects to your piping system is just as important as the valve itself. Selecting the correct end connection improves installation efficiency, minimises leakage risks, and simplifies future maintenance. Common connection types include: The best connection depends on your plant design, maintenance strategy, and operating conditions. Our team works with customers to recommend connection types that integrate seamlessly with existing systems while complying with Australian industry standards. Consider Manual or Automated Operation Modern industrial facilities increasingly rely on automation to improve productivity and operational safety. While manual lever-operated valves remain suitable for many applications, automated ball valves provide greater control where frequent operation or remote monitoring is required. Automation offers several advantages: Depending on your process requirements, actuators may be pneumatic, electric, or hydraulic. Selecting the correct actuator ensures reliable valve performance while supporting efficient plant operations. Think About Maintenance Before Installation A quality valve should not only perform well today but also remain reliable for years to come. When evaluating an industrial ball valve, consider its maintenance requirements throughout its service life. Look for features such as: Although premium valves may involve a higher initial investment, they often reduce maintenance costs and minimise unexpected downtime over the long term. Leakage Prevention Should Be a Priority Industrial facilities cannot afford product loss, environmental contamination, or safety hazards caused by valve leakage. Reliable sealing depends on multiple factors, including: High-performance valves are designed to maintain

How to Perform a Valve Audit: Ensuring Operational Safety & Efficiency

Industrial plants rely heavily on valves to control flow, pressure, temperature, and overall process stability. Over time, even well-designed valves can develop issues such as leakage, wear, incorrect calibration, or performance degradation. Without proper evaluation, these problems can lead to energy loss, safety risks, production inefficiencies, and unplanned downtime. A structured valve audit process helps engineers and operations teams assess valve condition, validate performance, and ensure systems are operating safely and efficiently. For reliability engineers and safety professionals, a valve audit is not just a maintenance activity, it is a critical part of operational risk management. Industrial operators can access advanced valve solutions and technical support through Flowlink EPL, which provides expertise in valve automation, instrumentation, and industrial process optimization. Understanding the Purpose of a Valve Audit A valve audit is a systematic evaluation of all valves within a facility to determine whether they are functioning correctly and efficiently. The goal is to identify performance gaps, detect leaks, assess wear and tear, and confirm whether each valve matches its intended operating conditions. A proper valve audit process focuses on: By addressing these factors, organizations can significantly improve safety, reduce operational costs, and extend equipment life. Step 1: Asset Identification and System Mapping The first stage of a valve audit process involves identifying all valves within the system and documenting their specifications. This includes valve type, size, pressure rating, material of construction, actuator type, and service application. Engineers also need to map each valve’s role in the process. Understanding whether a valve is used for isolation, regulation, or emergency shutdown helps determine its criticality. Accurate documentation is essential because incomplete asset data can lead to incorrect assessments and missed performance issues. This stage also creates a baseline for future audits and maintenance planning. Step 2: Reviewing Maintenance History Maintenance history provides valuable insight into valve reliability and long-term performance trends. Reviewing records helps identify recurring issues such as leaks, frequent repairs, or actuator malfunctions. Key aspects to evaluate include: A valve with repeated maintenance issues may indicate incorrect specification, poor installation, or unsuitable material selection. Understanding maintenance patterns allows engineers to prioritize critical valves and improve preventive maintenance strategies. Step 3: Visual Inspection and Condition Assessment Visual inspection is one of the most practical and effective stages of the valve audit process. It involves examining valves for external signs of damage or deterioration. During inspection, engineers typically look for: Environmental conditions play a significant role in valve degradation. Exposure to chemicals, moisture, high temperatures, or abrasive materials can significantly reduce valve lifespan if not properly managed. Step 4: Leak Detection and Energy Loss Evaluation Leaks are one of the most common and costly issues in industrial valve systems. They not only reduce process efficiency but also contribute to significant energy loss. A comprehensive valve audit process includes leak detection using methods such as: Even small leaks can lead to substantial energy waste over time, especially in steam, compressed air, and high-pressure systems. Identifying and repairing leaks improves efficiency and reduces operational costs. Step 5: Checking Correct Valve Specification Incorrect valve specification is a major cause of premature failure and poor performance. During the audit, engineers must verify whether each valve is suitable for its application. Key factors include: Material selection is especially critical in aggressive environments. Using incompatible materials can lead to corrosion, leakage, or mechanical failure. Correct specification ensures that valves operate efficiently and safely under expected conditions, reducing long-term maintenance requirements. Step 6: Performance Testing of Valves Performance testing evaluates whether valves function as intended under real operating conditions. This stage is essential for identifying hidden operational issues. Typical tests include: Performance testing ensures that valves respond correctly to control signals and maintain stable operation within process requirements. Step 7: Evaluating Materials and Wear Conditions Valve materials directly influence durability, reliability, and resistance to environmental stress. During the valve audit process, engineers assess whether materials are appropriate for the application. Factors such as corrosion resistance, abrasion resistance, and temperature tolerance are critical. Signs of material degradation include: If material incompatibility is detected, replacing or upgrading the valve may be necessary to ensure long-term reliability. Step 8: Risk and Criticality Analysis Not all valves have the same importance in a process system. Some valves directly impact safety, production continuity, or environmental protection. A criticality assessment helps categorize valves based on: Critical valves require more frequent inspection and monitoring to prevent high-risk failures. Tools Used in a Valve Audit Process Modern valve audits rely on advanced diagnostic tools to improve accuracy and efficiency. Common tools include: These tools help engineers detect issues that may not be visible during manual inspection, improving overall audit reliability. Industrial facilities can stay updated on advanced valve technologies and industry practices through Flowlink EPL News. Benefits of a Valve Audit Process A structured valve audit process delivers multiple operational advantages. It improves safety by identifying faulty or leaking valves before they become hazards. It reduces energy loss by detecting inefficiencies in fluid or gas systems. It also enhances reliability by ensuring valves operate within correct specifications. Additional benefits include: Overall, valve audits support long-term operational stability and cost control. Building a Continuous Valve Management Strategy A valve audit should not be treated as a one-time activity. Instead, it should be part of a continuous improvement strategy that includes regular inspections, predictive maintenance, and performance monitoring. Organizations should implement: This proactive approach ensures consistent system performance and reduces unexpected failures. For expert support in developing valve reliability strategies or selecting appropriate solutions, engineers can connect through. Conclusion Performing a valve audit process is essential for maintaining operational safety, reducing energy loss, and ensuring long-term system efficiency. By systematically evaluating maintenance history, checking for leaks, verifying correct specification, assessing materials, and conducting performance testing, engineers can significantly improve plant reliability. In modern industrial environments, where efficiency and safety are critical, valve audits are a key component of effective asset management. A well-structured audit process not only prevents failures but also enhances productivity and reduces operational costs over time. Frequently Asked Questions 1. What is

smart valve

Smart Valve Automation & Remote Monitoring: Trends & Benefits

Industrial automation is entering a new era. As digital transformation accelerates across manufacturing, oil & gas, water treatment, power generation, and process industries, traditional valve systems are evolving into intelligent, connected assets.For industrial automation and digital transformation teams, the question is no longer whether to modernize infrastructure — it’s how quickly to adopt smart solutions that deliver measurable returns. At the center of this shift is valve automation remote monitoring, powered by advanced sensors, cloud connectivity, and intelligent analytics. This pillar guide explores emerging technologies in smart valve automation, explains how IoT valve systems work, and provides a practical ROI-focused framework to support strategic investment decisions. The Evolution of Valve Automation Valves have always played a critical role in industrial processes. From regulating flow to ensuring system safety, components like pressure safety valves and butterfly valves are foundational elements of plant reliability. Traditionally, these valves operated mechanically or with basic actuators. Monitoring required manual inspections, scheduled maintenance, and reactive troubleshooting. While functional, this approach limited visibility and increased downtime risk. Today, intelligent automation is transforming these mechanical components into connected, data-driven assets. From Manual to Intelligent Control The journey has progressed through three main stages: This third stage — valve automation remote monitoring — is where digital transformation teams can unlock substantial performance gains. What Is Valve Automation Remote Monitoring? Valve automation remote monitoring refers to the integration of: Together, these components enable real-time visibility into valve performance, health status, and operational conditions — from anywhere in the world. Instead of relying solely on scheduled maintenance intervals, engineers can: This shift from reactive to predictive operations dramatically reduces operational risk. The Role of IoT Valve Technology An IoT valve is a connected valve equipped with sensors and communication capabilities that transmit performance data to centralized systems. Core Capabilities of IoT Valves IoT valves are not limited to a specific type. Whether deployed in high-pressure environments with pressure safety valves or used in flow control systems with butterfly valves, connectivity enhances reliability across applications. Emerging Technology Spotlight Digital transformation teams should pay close attention to several key innovations shaping smart valve automation. 1. Edge Computing for Faster Decisions Edge devices process data locally before transmitting to the cloud. This reduces latency and enables immediate responses to critical changes — especially important for high-risk systems. 2. AI-Powered Predictive Maintenance Machine learning models analyze historical valve behavior to identify failure patterns. Instead of waiting for a valve to seize or leak, systems flag subtle anomalies early. 3. Digital Twin Technology Digital twins replicate physical valve systems in virtual environments. Teams can simulate operating conditions, test performance scenarios, and forecast wear rates without disrupting operations. 4. Cybersecurity-Integrated Architecture As more IoT valve systems connect to enterprise networks, cybersecurity becomes critical. Modern platforms include encryption, role-based access controls, and intrusion detection to protect infrastructure. 5. Cloud-Based Asset Dashboards Centralized dashboards allow multi-site organizations to monitor thousands of valves in a single interface — driving enterprise-wide visibility and consistency. Business Case: ROI Analysis for Smart Valve Automation For digital transformation leaders, investment decisions require clear financial justification. Fortunately, valve automation remote monitoring delivers measurable returns across multiple areas. 1. Reduced Unplanned Downtime Unplanned downtime is one of the largest hidden costs in industrial environments. A single valve failure can: Predictive maintenance reduces emergency shutdowns and extends equipment life. ROI Driver: Even a 10–20% reduction in downtime can result in substantial annual savings. 2. Lower Maintenance Costs Traditional maintenance often relies on fixed schedules, regardless of actual wear. This results in: IoT valve monitoring enables condition-based maintenance — servicing valves only when needed. ROI Driver: Reduced labor hours and spare parts consumption. 3. Improved Energy Efficiency Valves that do not operate at optimal calibration can increase energy consumption. Minor leaks or improper positioning can create major inefficiencies over time. Smart automation ensures: ROI Driver: Lower utility costs and improved sustainability metrics. 4. Extended Asset Lifecycle Real-time performance insights prevent premature wear. By addressing minor issues early, organizations can extend the lifespan of: ROI Driver: Deferred capital expenditures on replacement equipment. 5. Enhanced Safety & Compliance In industries where safety is paramount, valve failure can have catastrophic consequences. Remote monitoring provides: ROI Driver: Reduced liability risk and improved regulatory compliance. Integration Strategy for Digital Transformation Teams Implementing valve automation remote monitoring requires strategic planning. Step 1: Asset Assessment Identify critical valves that: Prioritize these assets for IoT upgrade. Step 2: Infrastructure Readiness Ensure compatibility with: Modern IoT valve systems are designed for seamless integration. Step 3: Pilot Deployment Start with a controlled pilot project: This data becomes the foundation for enterprise-scale ROI justification. Step 4: Scale Strategically After validating performance improvements, expand deployment across: Key Industry Applications Valve automation remote monitoring is transforming industries such as: Across all sectors, digital transformation teams are prioritizing smart infrastructure to increase resilience and operational agility. Operational Benefits Beyond Cost Savings While ROI is critical, strategic advantages extend further. Real-Time Visibility Executives and plant managers gain immediate insight into asset performance. Data-Driven Decision Making Performance trends inform capital planning and maintenance strategy. Workforce Optimization Technicians spend less time on manual inspections and more on high-value tasks. Sustainability Alignment Improved efficiency reduces emissions and resource waste. Overcoming Common Implementation Challenges Concern: High Initial Investment While upfront costs exist, long-term savings often offset investment within 12–24 months. Concern: Integration Complexity Modern platforms are designed for interoperability with existing industrial systems. Concern: Cybersecurity Risks Advanced encryption and network segmentation protect connected valve infrastructure. Future Outlook: The Next Phase of Smart Valve Automation The next five years will likely bring: Organizations that invest early will build competitive advantage through operational intelligence. Why Strategic Partnerships Matter Selecting the right partner is essential. Companies like Flowlink Valves & Controls understand both traditional valve engineering and emerging digital technologies. By combining expertise in pressure safety valves, butterfly valves, and advanced automation systems, strategic partners help digital transformation teams bridge the gap between mechanical infrastructure and intelligent connectivity. The goal is not just automation — but scalable, measurable performance

pressure valves

Back Pressure Valves in Oil and Gas Systems Ensuring Safety and Flow Control

Back pressure valve oil and gas applications play a critical role in maintaining controlled pressure levels across complex pipeline and processing systems. In environments where fluids and gases move through interconnected equipment under varying operating conditions, pressure stability is essential for safety, efficiency, and system longevity. Engineers, safety officers, and system designers rely on precisely engineered back pressure valves and safety valves to ensure controlled flow, predictable performance, and protection of downstream components. Within oil and gas facilities pressure fluctuations can originate from changes in flow demand equipment cycling temperature variation or operational sequencing. Without effective pressure regulation these fluctuations may compromise system integrity and process control. Back pressure valves function as a primary pressure regulating element designed to maintain a predetermined upstream pressure regardless of downstream variations. Understanding the Engineering Principles of Back Pressure Valves Back pressure valves are designed to regulate upstream pressure by restricting flow when pressure exceeds a set value. Unlike simple check valves which permit flow in only one direction back pressure valves actively modulate flow based on pressure conditions. Their operation relies on calibrated spring mechanisms pilot control systems or diaphragm based designs that respond directly to pressure changes. When upstream pressure rises above the valve set point the internal mechanism adjusts to create resistance. This resistance stabilizes pressure and ensures consistent flow conditions. Once pressure returns to acceptable levels the valve opens accordingly allowing normal system operation. This self regulating behavior makes back pressure valves indispensable in oil and gas systems where pressure balance is essential. Engineering design considerations include response sensitivity material compatibility and sealing performance. Valves must withstand corrosive fluids high temperatures and continuous duty cycles. Precision in design ensures accurate pressure regulation without excessive wear or instability. Role of Back Pressure Valves in Oil and Gas Safety Mechanisms Safety mechanisms within oil and gas infrastructure depend heavily on controlled pressure management. Excessive pressure can lead to equipment damage, seal failure, or unsafe operating conditions. Flowlink back pressure valves provide a passive yet reliable safeguard by preventing pressure escalation before it reaches critical levels. In upstream operations these valves protect separators and pumps by maintaining steady inlet conditions. In midstream transport systems they ensure pipeline stability and reduce stress on joints and fittings. Downstream processing facilities benefit from consistent pressure that supports accurate flow measurement and process efficiency. Unlike emergency relief devices that activate only during abnormal events back pressure valves operate continuously as part of normal system control. This proactive approach enhances overall safety by reducing reliance on reactive safety responses. Integration with Check Valves and Flow Control Valves Back pressure valves often function alongside check valves and flow control valves within integrated systems. Each component serves a distinct yet complementary role. Check valves prevent reverse flow protecting pumps and compressors from backflow damage. Flow control valves regulate volumetric flow rates ensuring balanced distribution across the system. Back pressure valves add a layer of pressure regulation that stabilizes upstream conditions. Together these components create a controlled environment where pressure flow direction and volume remain within engineered limits. Proper integration ensures smooth transitions during startup shutdown and load changes. System designers must consider valve placement and interaction to avoid oscillation or unintended pressure buildup. Coordinated valve selection ensures optimal performance and long term reliability. Pressure Regulation Across Complex Oil and Gas Networks Pressure regulation is a continuous challenge in oil and gas operations due to long distances, multiple processing stages, and variable demand. Flowlink back pressure valves help maintain equilibrium across these networks by isolating pressure zones and preventing downstream disturbances from affecting upstream equipment. In gas processing applications pressure stability supports accurate separation and conditioning processes. In liquid transport systems regulated pressure reduces cavitation risk and protects pumps. By maintaining consistent upstream pressure back pressure valves enhance predictability across the entire network. This stability improves operational control and reduces the likelihood of maintenance related disruptions. Engineers value back pressure valves for their ability to maintain equilibrium without requiring constant manual intervention. Performance Benefits of Back Pressure Valve Oil and Gas Applications The performance benefits of back pressure valve oil and gas systems extend beyond basic pressure control. These valves contribute to improved equipment lifespan by minimizing pressure induced stress. Reduced pressure fluctuation leads to fewer seal failures and lower maintenance demands. Operational efficiency also improves when pressure remains consistent. Flow measurements become more accurate and process control systems function more effectively. This consistency supports optimized production without compromising safety. Another key benefit is system adaptability. Back pressure valves respond automatically to changing conditions allowing systems to handle variable flow scenarios without manual adjustment. This adaptability is especially valuable in remote or automated oil and gas installations. Material and Design Considerations for Harsh Environments Oil and gas systems operate in demanding environments where valves must endure corrosion erosion and temperature extremes. Back pressure valves are engineered using materials selected for compatibility with hydrocarbons gases and process chemicals. Internal components require precision machining to maintain sealing integrity under pressure. Surface finishes and coatings enhance durability while reducing friction. These design elements ensure reliable performance over extended operational cycles. System designers prioritize valves that combine robust construction with precise control characteristics. High quality engineering minimizes leakage risk and maintains consistent pressure regulation even under continuous operation. Flowlink Innovations in Back Pressure Valve Technology Flowlink has advanced back pressure valve oil and gas solutions through a focus on precision engineering reliability and system integration. Flowlink valves are designed to deliver consistent pressure regulation while adapting to complex operating conditions. Innovations include refined internal geometries that improve response accuracy and reduce wear. Enhanced sealing technologies support long term pressure stability while minimizing maintenance requirements. Flowlink designs also emphasize ease of integration within existing systems allowing engineers to upgrade pressure control without extensive modifications. By aligning valve performance with real world operational demands Flowlink supports safer and more efficient oil and gas infrastructure. Their engineering approach reflects a commitment to dependable pressure regulation and system protection. Selecting the Right Back Pressure Valve for Your System

Why Choosing the Right Valves for the Oil and Gas Industry Matters

Selecting the correct valves is one of the most important decisions in any oil and gas operation. At Flowlink Valves & Controls, we understand that the right valve can significantly affect operational efficiency, safety, and overall system performance. The choices you make in valves for the oil and gas industry influence the functionality of pipelines and equipment, compliance with safety standards, and long-term reliability. Working with trusted oil and gas valves manufacturers ensures that your systems operate safely and efficiently. In this article, we explore the importance of proper valve selection, the types available, and expert guidance to ensure your oil and gas systems perform optimally. Understanding Valves in Oil and Gas Operations Valves are fundamental components in oil and gas infrastructure. They regulate the flow of liquids and gases under varying pressures and temperatures, ensuring operational safety and efficiency. Choosing the right valve ensures reliable operation, minimises maintenance issues, and prevents costly downtime. Valves are not merely functional devices; they are critical safety and efficiency elements. The wrong choice can result in frequent failures, increased maintenance, and even safety hazards. For engineers, project managers, and procurement teams, understanding valve functionality is the first step towards optimising operations. Partnering with reputable oil & gas valve manufacturers guarantees compliance with industry standards and access to high-quality products. Key Functions of Industrial Valves Valves perform several critical roles in oil and gas operations: Flow Control: They regulate the movement of oil, gas, or other fluids within pipelines and processing systems. Efficient flow control ensures that production processes operate smoothly and safely. Pressure Regulation: Valves maintain system integrity by controlling and stabilising pressure, preventing damage to pipelines and connected equipment. Safety Assurance: Valves can isolate sections of pipelines to prevent leaks, spills, or hazardous incidents, which is essential for meeting safety and environmental standards. Operational Efficiency: Reliable valves reduce downtime and increase productivity by ensuring consistent performance, enabling smoother day-to-day operations. Types of Valves Used in the Oil and Gas Industry The oil and gas sector requires specialised valves designed to handle high pressure, extreme temperatures, and corrosive fluids. Choosing the right type of valve is critical to maintaining safety and efficiency. Below is a detailed look at commonly used valve types from trusted oil and gas valves manufacturers: Valve Type Function Common Applications Advantages Ball Valve On/off control Pipelines, storage tanks Quick operation, minimal leakage, high durability Gate Valve Full flow or isolation Wellheads, refineries Long-lasting, low-pressure drop, suitable for high-pressure systems Globe Valve Flow regulation Pressure control systems Precise flow control, excellent throttling capabilities Check Valve Prevent backflow Pump systems, pipelines Simple, reliable, prevents reverse flow and system damage Back Pressure Valve Maintain pressure Separator systems, downstream equipment Protects equipment, ensures consistent pressure Why Ball Valves Are Preferred A ball valve for oil and gas industry operations is a popular choice because it offers rapid opening and closing, excellent sealing, and the ability to handle high pressures and temperatures. Their design ensures minimal leakage and reduces maintenance needs. This makes them particularly suitable for critical points in pipelines, storage systems, and high-pressure operations. Additional Valve Considerations When choosing valves, engineers must consider: Flow Type: Is the fluid gas, liquid, or multiphase? Some valves perform better with gas, while others are designed for liquid or mixed-phase flow. Environmental Conditions: Extreme temperatures, corrosive fluids, or offshore conditions require specialised valve materials and coatings. Valve Operation Frequency: High-use valves need designs that can endure repeated operation without degradation. Manufacturer Reputation: Partnering with reliable oil & gas valve manufacturers ensures that valves meet strict quality and safety standards. Factors to Consider When Selecting Valves Selecting the right valve requires careful evaluation of multiple technical and operational factors. Making informed choices ensures system reliability, safety, and performance. Material Compatibility Valves must withstand corrosion, erosion, and wear caused by transported fluids. Stainless steel, carbon steel, and specialised alloys are commonly used in oil and gas operations. Correct material selection reduces the risk of early failure and ensures long-term reliability, even in challenging environments. Working with leading oil and gas valves manufacturers can help ensure material compatibility and durability. Pressure and Temperature Ratings Every system has specific pressure and temperature requirements. Valves must meet or exceed these parameters to prevent leaks, operational interruptions, or equipment failure. A valve that cannot handle system conditions may result in premature wear or safety hazards. Back pressure valves in oil and gas operations are particularly important for maintaining stable pressure and protecting downstream equipment. Reliability and Maintenance Valves are long-term investments. Selecting durable, low-maintenance valves improves operational efficiency and reduces unplanned downtime. Reliability is particularly important in remote or offshore installations, where maintenance access can be difficult and costly. Choosing trusted oil and gas valves manufacturers ensures access to products designed for high reliability. Industry Compliance and Safety Standards Valves must comply with recognised standards, such as API, ISO, and ASME, to ensure safe operation. Compliance ensures that systems are legally compliant and safe for personnel and the environment. Certified valves from reputable oil & gas valve manufacturers support operational assurance in complex industrial operations. Installation and Compatibility Even the best valve can fail if it is not properly installed or compatible with the system layout. Engineers must consider pipe diameter, system flow rate, and connection types. This ensures the valve operates correctly and integrates smoothly with existing infrastructure. How the Right Valve Improves Efficiency Proper valve selection directly improves operational efficiency. Some key benefits include: Reduced Downtime: Durable valves from reliable oil and gas valves manufacturers minimise the need for frequent replacements or maintenance. Energy Savings: Efficient flow control reduces pumping energy requirements, contributing to operational efficiency and sustainability. Process Accuracy: Correct valves ensure precise flow and pressure regulation, which is vital for complex production processes. Safety and Reliability: Using the right valves maintains system integrity, reduces the risk of leaks or failures, and supports safe operations. Operational efficiency is not just about productivity; it also ensures compliance with safety regulations, reduces operational risk, and improves overall system longevity. Common

How Ball Valves Power the Oil and Gas Industry: Design, Performance, and Reliability Explained

In the oil and gas industry, precision, reliability, and durability are crucial. Every component in the system must perform flawlessly under high pressure, extreme temperatures, and challenging operational conditions. Among these components, ball valves for oil and gas industry applications play a pivotal role. At Flowlink Valves & Controls, we specialise in providing high-quality valves designed to meet the demanding requirements of oilfield operations. In this article, we’ll explore how oil and gas valves manufacturers like Flowlink Valves & Controls engineer ball valves for optimal performance, examine their design features, and explain why they are essential for safe and efficient oil and gas operations. Understanding Ball Valves in the Oil and Gas Industry Ball valves are among the most widely used valves in the oil and gas sectors. Their design allows for quick, reliable shutoff, making them ideal for critical operations where safety and efficiency are paramount. What Are Ball Valves? A ball valve is a quarter-turn valve that uses a spherical disc to control the flow of liquids or gases. By rotating the ball 90 degrees, the valve either allows full flow or completely stops it. This simple mechanism provides several advantages: Rapid operation for emergency shutoff Minimal leakage when closed Long service life with low maintenance Ball valves are available in different types, including trunnion-mounted ball valves and floating ball valves, each suited to specific pressure and operational requirements. Applications in the Oil and Gas Sector Ball valves are essential at various stages of oil and gas operations: Upstream: Used in exploration, drilling, and production facilities to control crude oil and natural gas flow. These valves must withstand high-pressure conditions, abrasive fluids, and extreme temperatures. Midstream: Critical in pipelines and transportation systems, ensuring pressure control, safety, and uninterrupted flow. Back pressure valves for oil and gas applications are often used to maintain steady pressure levels. Downstream: Used in refineries and processing plants for chemical handling and fluid control. These valves handle high temperatures and corrosive materials, ensuring the safe operation of complex refining processes. Due to their versatility, valves for oil and gas industry applications must meet strict standards for durability, pressure tolerance, and chemical resistance. Operators rely on manufacturers that can deliver precision-engineered solutions tailored to each stage of the oil and gas value chain. Key Design Features of Flowlink Valves & Controls Ball Valves At Flowlink Valves & Controls, our valves are engineered to perform reliably in high-pressure oilfield environments. Understanding these design features helps explain why they are the preferred choice for many operators. Trunnion-Mounted vs Floating Ball Valves Choosing the right type of ball valve depends on the application, pressure, and operational needs. Here’s a comparison: Feature Trunnion-Mounted Ball Valve Floating Ball Valve Support Ball supported by trunnions (top and bottom) Ball supported by valve seats only Pressure Handling Suitable for high-pressure applications Suitable for moderate-pressure applications Torque Requirement Lower torque for operation Higher torque required Maintenance Easier to maintain in large systems Moderate maintenance required Trunnion-mounted valves are ideal for pipelines with very high pressures, while floating ball valves are preferred for standard applications with moderate flow rates. Operators often select based on pipeline diameter, system pressure, and the specific type of fluid being handled. Advanced Valve Sealing Effective sealing is critical in oil and gas operations to prevent leaks and maintain system safety. Flowlink Valves & Controls’ ball valves for oil and gas industry use a combination of sealing technologies: Soft seats: Provide tight sealing and minimise leakage. Soft seats are commonly used in low- to medium-pressure applications where precise shutoff is required. Metal-to-metal seals: Offer durability in extreme temperatures and high-pressure conditions, making them suitable for upstream oilfield operations. Back-up seals: Maintain performance in high-pressure operations and ensure reliability over long service periods. These are particularly valuable in offshore and subsea installations where maintenance opportunities are limited. Material Selection for Durability Materials must withstand corrosive fluids, abrasive media, and high temperatures. Flowlink Valves & Controls’ valves are crafted from: Stainless steel for chemical resistance Alloy steels for high-pressure pipelines Special coatings for enhanced longevity and protection against erosion The careful selection of materials ensures that Flowlink Valves & Controls valves meet international safety and durability standards, making them a preferred choice among oil & gas valve manufacturers worldwide. Performance and Reliability in Oilfield Operations Performance is a critical factor in the oil and gas industry. A poorly performing valve can cause downtime, reduce productivity, and even pose safety risks. Pressure Control Capabilities Maintaining precise pressure control is essential in pipelines and process systems. Back pressure valves for oil and gas applications help maintain system stability by preventing surges, pressure spikes, and unplanned downtime. For example, in midstream pipelines, even minor pressure fluctuations can compromise flow efficiency and increase the risk of pipeline fatigue. Durability in Harsh Environments Flowlink Valves & Controls valves are designed to withstand: Abrasive fluids and gases that can erode conventional valve components Extreme temperatures ranging from sub-zero conditions in Arctic pipelines to temperatures exceeding 200°C in refinery processes High-cycle operations for frequent start-stop sequences, ensuring long-term reliability These features reduce maintenance needs, extend operational life, and enhance process safety, which is why they are preferred by engineers and plant operators across the oil and gas sector. Safety and Compliance All Flowlink Valves & Controls valves comply with stringent safety and industry standards. They are tested for: High-pressure tolerance Leak-tight sealing under demanding conditions Operational reliability across varied fluid types Compliance with safety standards ensures operators can rely on these valves in sensitive oil and gas operations, reducing the risk of environmental hazards and operational downtime. Choosing the Right Ball Valve for Your Operation Selecting the correct valve is essential for system efficiency, safety, and longevity. Key Considerations When selecting a ball valve, consider: Pressure rating: Match the valve to pipeline and process pressures. Temperature tolerance: Ensure materials can handle operational extremes. Valve type: Choose between floating or trunnion-mounted based on pressure requirements. Maintenance and accessibility: Factor in ease of installation and servicing, especially in remote or

We offer Engineering support and a complete suite of Engineered products for all your plant and flow control applications.

Operations & Warehouse

Follow Us